Attribute Inspection
Meaning ~ Binary quality control protocols categorize production units as conforming or non-conforming to determine the acceptance or rejection of manufacturing lots.
Classification
The Binary Decision Model
Binary evaluation protocols sort manufactured units strictly into conforming or non-conforming categories, forming the foundation of attribute inspection under standards like ISO 2859-1 to determine whether entire production lots pass or fail based on sample defect counts. The judgment is binary: a part fits into the ring gauge or it does not, and a surface is either free of scratches under standard lighting or defective. This pass-fail structure speeds up inspection because the examiner takes no continuous measurements.
Variables inspection, by comparison, requires calibrated instruments to capture numerical values in millimeters or grams. While variables data helps track process control, it evaluates only one characteristic at a time; an inspector checking a molded plastic connector can verify twenty distinct features at once using attribute inspection, whereas a variables protocol demands twenty separate measurements with distinct limits.
Boundary of Variable Measurements
Where attribute screening gives way to variables measurement comes down to gauge limitations and data collection costs. High-value automotive components or medical instruments demand variables inspection to track drift before parts fail, while consumer goods, apparel, and structural fasteners rely on pass or fail checks to screen bulk shipments quickly. A contract clause stipulating that all testing will proceed under ISO 2859-1 normal level II, and that any shift to tightened level II shifts all re-inspection costs to the supplier, immediately changes the structure of pre-shipment quality negotiations.
Risk
Acceptable Quality Limit Calibration
Sampling plans established under statistical standards determine the probability of accepting a lot with a given proportion of non-conforming items. The Acceptable Quality Limit defines the poorest process average a buyer considers acceptable for sampling purposes, rather than a license to ship defective goods. Under general inspection level II, a lot of five thousand units maps to code letter L and requires a fixed sample size of two hundred units.
A lot of five thousand units evaluated at level II with a major defect limit of one percent demands a sample size of two hundred units.
Drawing sample units randomly across the lot preserves statistical validity. If the sample of two hundred contains seven or fewer non-conforming units, the lot passes; eight or more non-conforming units leads to rejection under standard table parameters.
- attribute inspection schedules employ randomized sampling across the batch to reflect the overall quality of the production run.
- attribute inspection calculations, based on operating characteristic curves, establish the risk profiles for both the buyer and the supplier before manufacturing begins.
- attribute inspection plans remain straightforward: once the buyer sets the acceptable quality level, standardized tables establish the required sample size alongside acceptance and rejection numbers.
| Lot Size | Code Letter | Sample Size | Acceptance Number (Ac) | Rejection Number (Re) |
|---|---|---|---|---|
| 281 to 500 | H | 50 | 1 | 2 |
| 501 to 1,200 | J | 80 | 3 | 4 |
| 1,201 to 3,200 | K | 125 | 5 | 6 |
| 3,201 to 10,000 | L | 200 | 7 | 8 |
| Source: ANSI/ASQ Z1.4-2008 Normal Single Sampling Plan. | ||||
How Does Lot Size Affect Sample Costs?
As the total order quantity grows, the sample size does not increase proportionally. The statistical power of the sample depends on its absolute size rather than the percentage of the lot inspected. For a lot size of one thousand units, code letter J demands eighty units under level II.
If the lot size increases to ten thousand, code letter L demands two hundred units. While the production volume increases tenfold, the sample size increases by only two and a half times. The buyer is left to ponder whether the statistical margin of safety provided by a single-sample plan of eighty units outweighs the possible administrative delay of a double-sampling schedule.
Bench
Physical Go/No-Go Fixtures
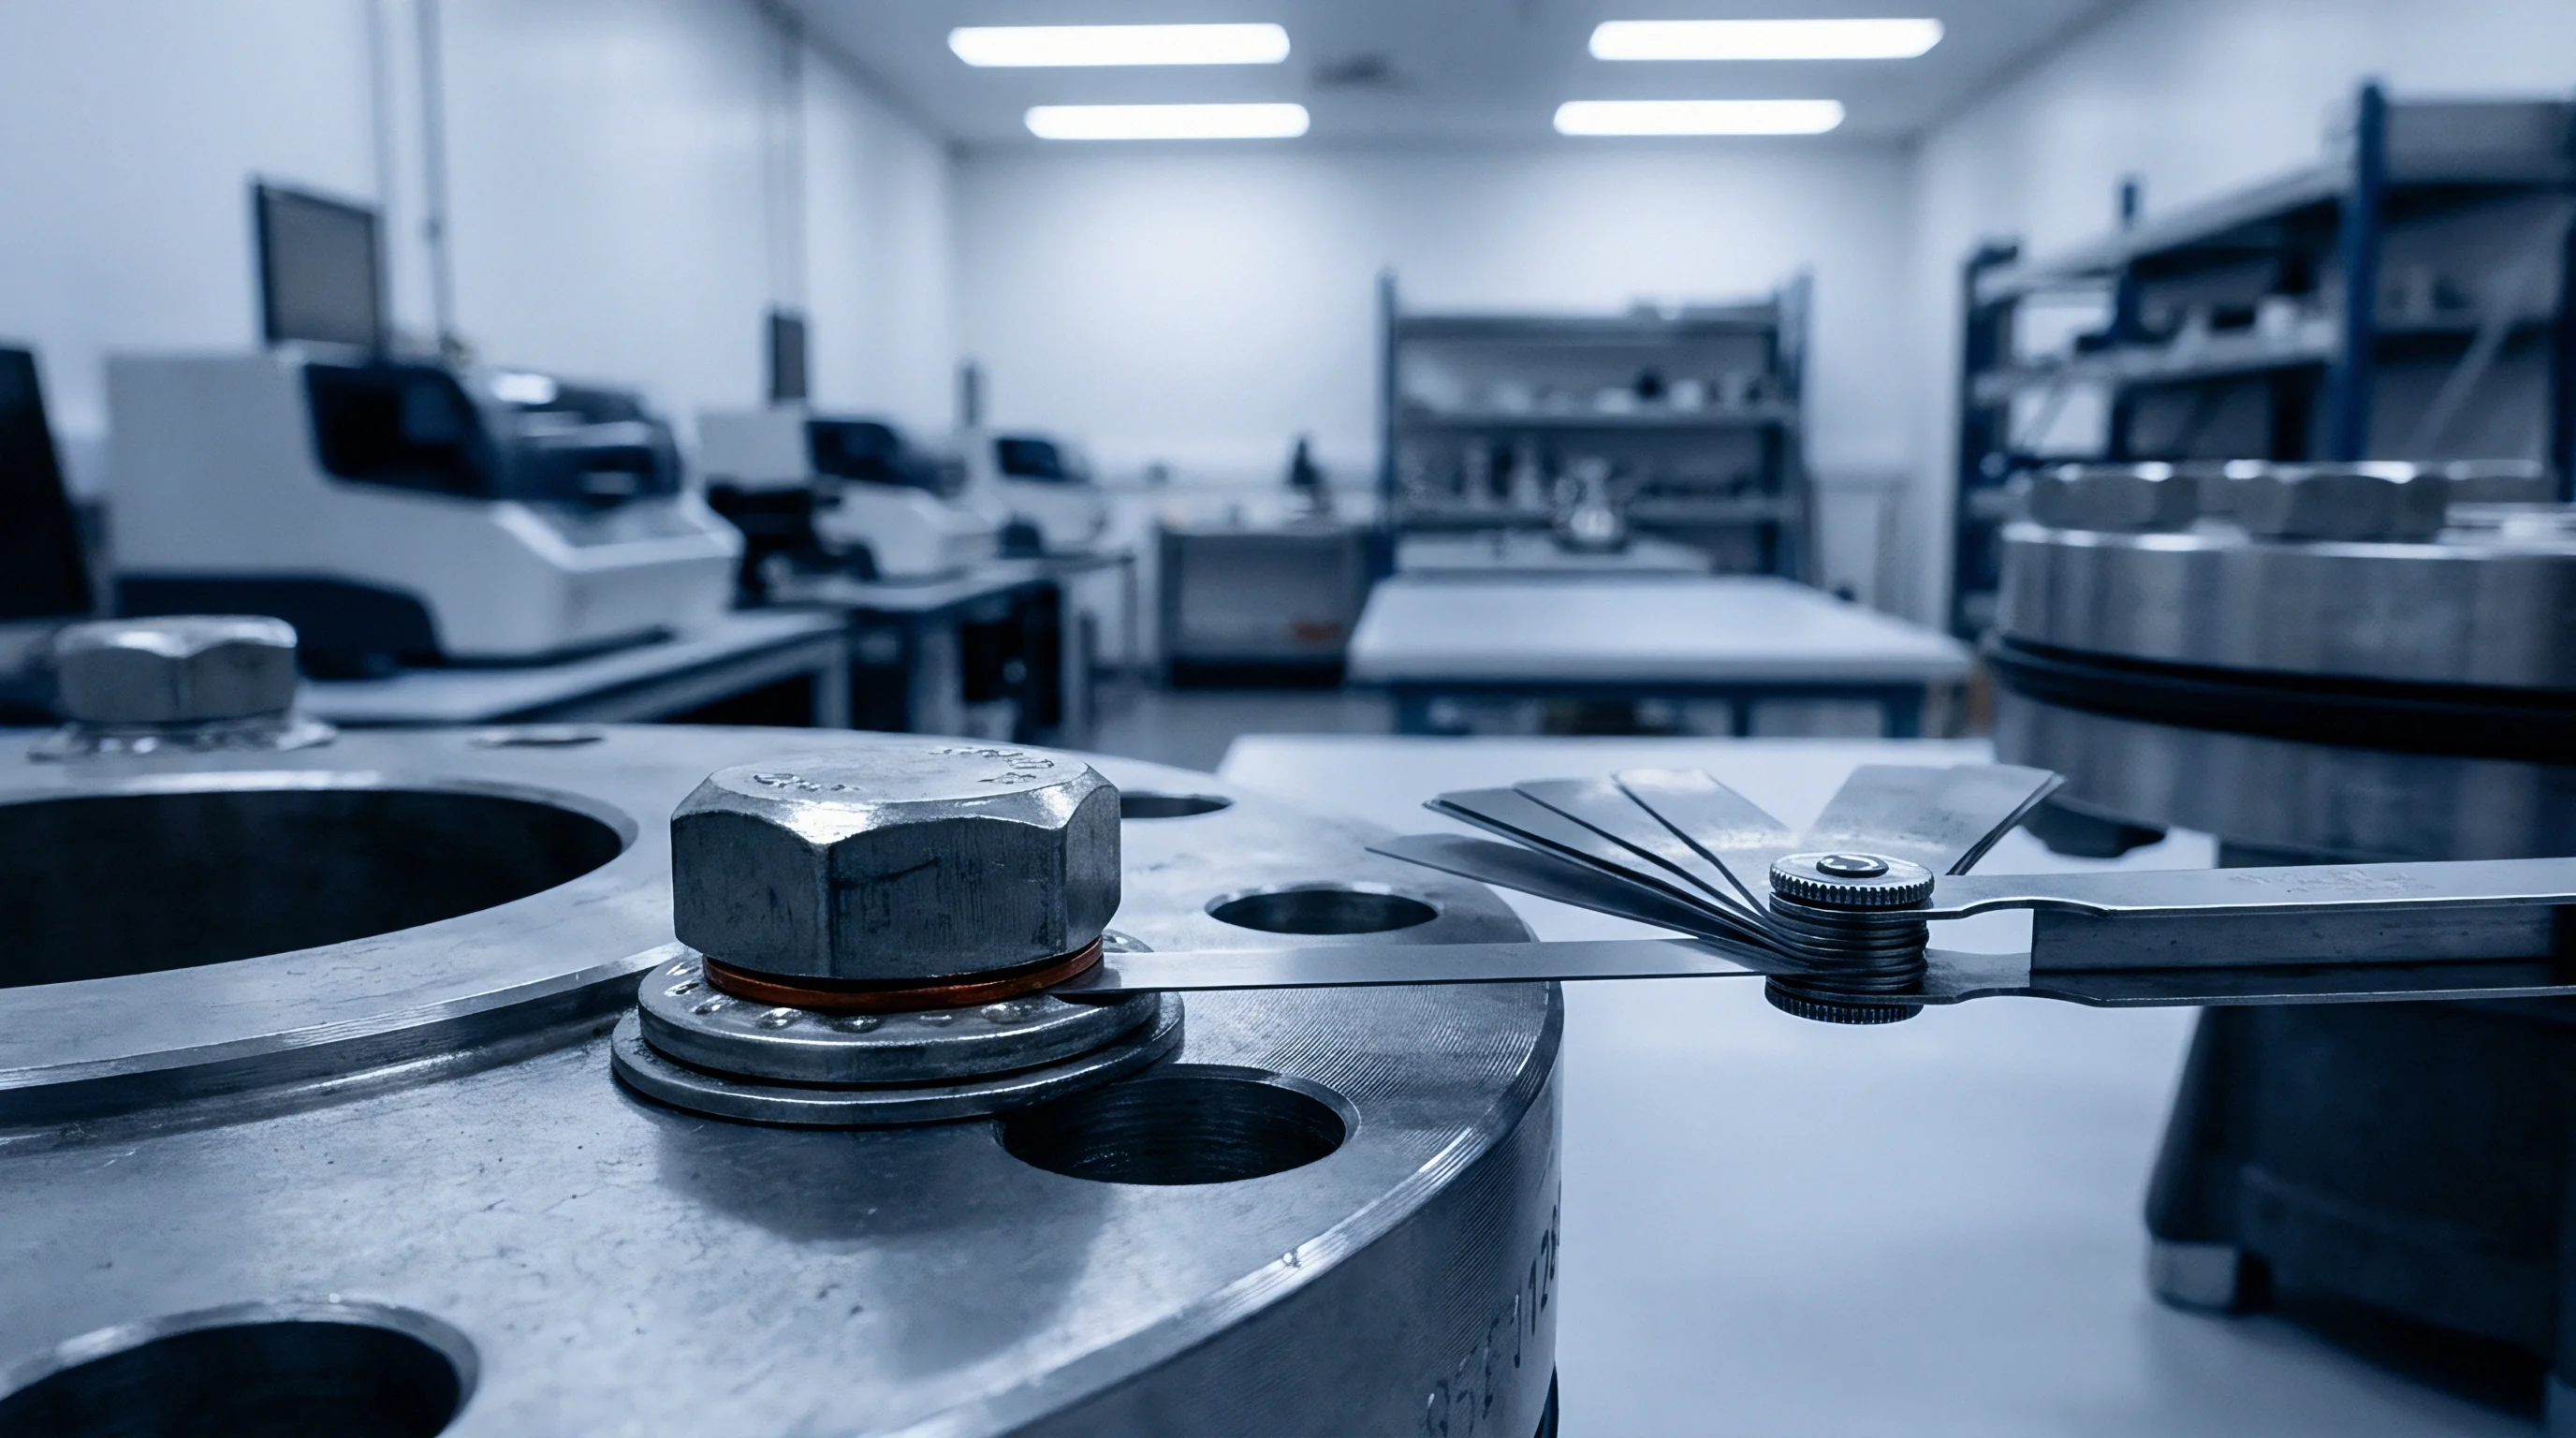
Executing pass-fail checks on the shop floor requires clear visual baselines, physical go/no-go gauges, or standardized test fixtures. When evaluating machined metal pins, an inspector uses a thread ring gauge: the go side engages smoothly with the pin while the no-go side does not fit, creating a purely mechanical boundary that removes subjectivity from the process. Visual inspections require physical master boards signed by both parties to define the threshold of acceptable finish, which are then locked on the factory floor.
The Cartons Drawing Protocol
Dedicated fixtures screen multiple characteristics in a single motion: a custom block gauge can verify both the length and width of a metal bracket simultaneously, keeping bench checks rapid and data recording simple.
- The inspector identifies the production lot and counts the total number of packed cartons.
- Random cartons are drawn from the batch based on the sampling plan’s sample size code letter.
- Each selected unit is evaluated using fixed gages or visual standards to determine conformity.
- Defect totals are compared directly to the acceptance and rejection numbers to decide the fate of the lot.
Inspectors pull samples from throughout the lot rather than taking them from the most accessible outer cartons, drawing across multiple pallet layers to accurately represent the entire run. Scratches on metal housings often occur during manual packing after assembly quality gates have cleared, creating disputes over whether handling marks compromise final acceptance.
Ledger
Amortizing the Tooling Cost
Comparing the economics of measuring physical variables against verifying binary characteristics determines the total cost of a quality assurance program. While a variables program requires expensive digital instruments and automated data logging systems, an attribute program operates with simple manual tools. Ring gauges, block fixtures, and visual masters cost relatively little to manufacture: a single-pin variables caliper can cost three hundred dollars, whereas a set of go/no-go gauges is bought for fifty dollars and amortizes across long production runs.
Gauges with fixed limits speed up evaluation work and remove operator bias from the floor.
| Cost Component | Attribute Verification (Ring Gage) | Variable Measurement (Caliper) |
|---|---|---|
| Required Sample Size | 200 units | 50 units |
| Evaluation Time per Unit | 5 seconds | 45 seconds |
| Total Evaluation Labor | 0.28 hours | 0.63 hours |
| One-time Tooling Cost | USD 150 | USD 350 |
| Total Cost per Batch | USD 164 | USD 382 |
| Summary Row | Lowest ongoing unit cost | Highest information yield |
Calculating the Total Economic Exposure
The true cost of quality extends well past labor hours alone to include the expense of accepting defective units that cause failures downstream. Variables inspection takes more time per part but flags process drift before dimensions fall out of spec. Attribute inspection, by contrast, gives its first warning only after the line has already produced out-of-tolerance units.
Selecting a sample that is too small to resolve a marginal defect rate can result in the high-cost scenario of receiving thousands of unusable assemblies at the assembly plant across the ocean.
Paperwork
Integrating Standards into Purchase Orders
Contracts governing industrial supply agreements specify the standard to be used for acceptance sampling and the party responsible for third-party evaluation costs. The purchase order serves as the legal vehicle holding the supplier to statistical standards; vague lines like goods shall be high quality carry no weight in an international dispute. Instead, referencing the exact sampling plan, inspection level, and AQL limits creates a binding framework that allows the buyer to reject non-conforming shipments and assign transport costs to the supplier.
The standard ISO 2859-1 allows the buyer to return the entire shipment if the defect count exceeds the rejection limit.
- attribute inspection specifications allocate the cost of re-inspection to the supplier if the lot fails the initial test.
- attribute inspection standards, such as ANSI/ASQ Z1.4, govern the evaluation criteria. Both parties agree to abide by these statistical rules.
- attribute inspection documentation, including signed quality agreements, prevents disputes over subjective defects on the assembly line.
Allocating Rejection Liability
When a production lot fails inspection, the buyer holds the right to reject the entire batch. Rejection triggers a cascading series of expenses, including storage fees, freight costs for returns, and manufacturing delays, which the supply contract must allocate. The simpler the tool required to verify a part, the more likely the inspector and the line operator will arrive at the identical quality verdict.
Friction
Resolving Defect Classification Arguments
Disagreements between buyers and suppliers often arise when borderline cosmetic issues are evaluated differently by inspectors at the factory and buyers at destination. Defects are categorized into hazard, major, and minor classes: hazard defects prevent safe use, major defects prevent normal function, and minor defects are cosmetic imperfections. Disagreements typically center on the boundary between minor and major defects.
A scratch on a remote control housing is cosmetic, but if it sits directly over the lock icon and renders it illegible, it becomes major, requiring objective baseline standards to settle.
Cosmetic defects on plastic housings generate the most intense arguments between quality control staff and factory managers.
- attribute inspection disputes arise when the definition of a major defect is left open to interpretation.
- attribute inspection tolerances limit the buyer’s risk of receiving a high proportion of cosmetic defects. They act as a defensive shield.
- attribute inspection registers record every borderline failure to build a historical quality profile of the supplier.
The Dispute Resolution Clause
An effective contract includes a clause to resolve these standoffs by specifying that disputed cosmetic defects will be evaluated by a third-party laboratory against the signed master boards, with the losing party paying for the tests. Storing verified physical master boards signed by both parties directly on the production floor minimizes the frequency of such disputes.
Tolerance
The Limits of Pass Fail Data
Sampling by attributes has structural limits: it cannot show how close a process is to failing, only whether a sampled unit has crossed into defect. Because attribute plans cannot measure capability indices or the standard deviation of critical dimensions, tracking tool wear or process drift requires more than attribute inspection alone. If a drill bit slowly wears down, the hole diameter shrinks gradually; an attribute pin gauge will pass the holes until the tool binds or breaks, by which point an entire batch may already be scrap.
Statistical Power and Field Failures
To detect defect rates as low as one hundred parts per million, attribute sampling requires sample sizes of thousands of units, which is economically unfeasible for most medium-volume orders. Thus, attribute sampling cannot guarantee the absence of low-frequency defects. The buyer secures long-term quality by coupling attribute filters with periodic lab tests of materials and dimensions.