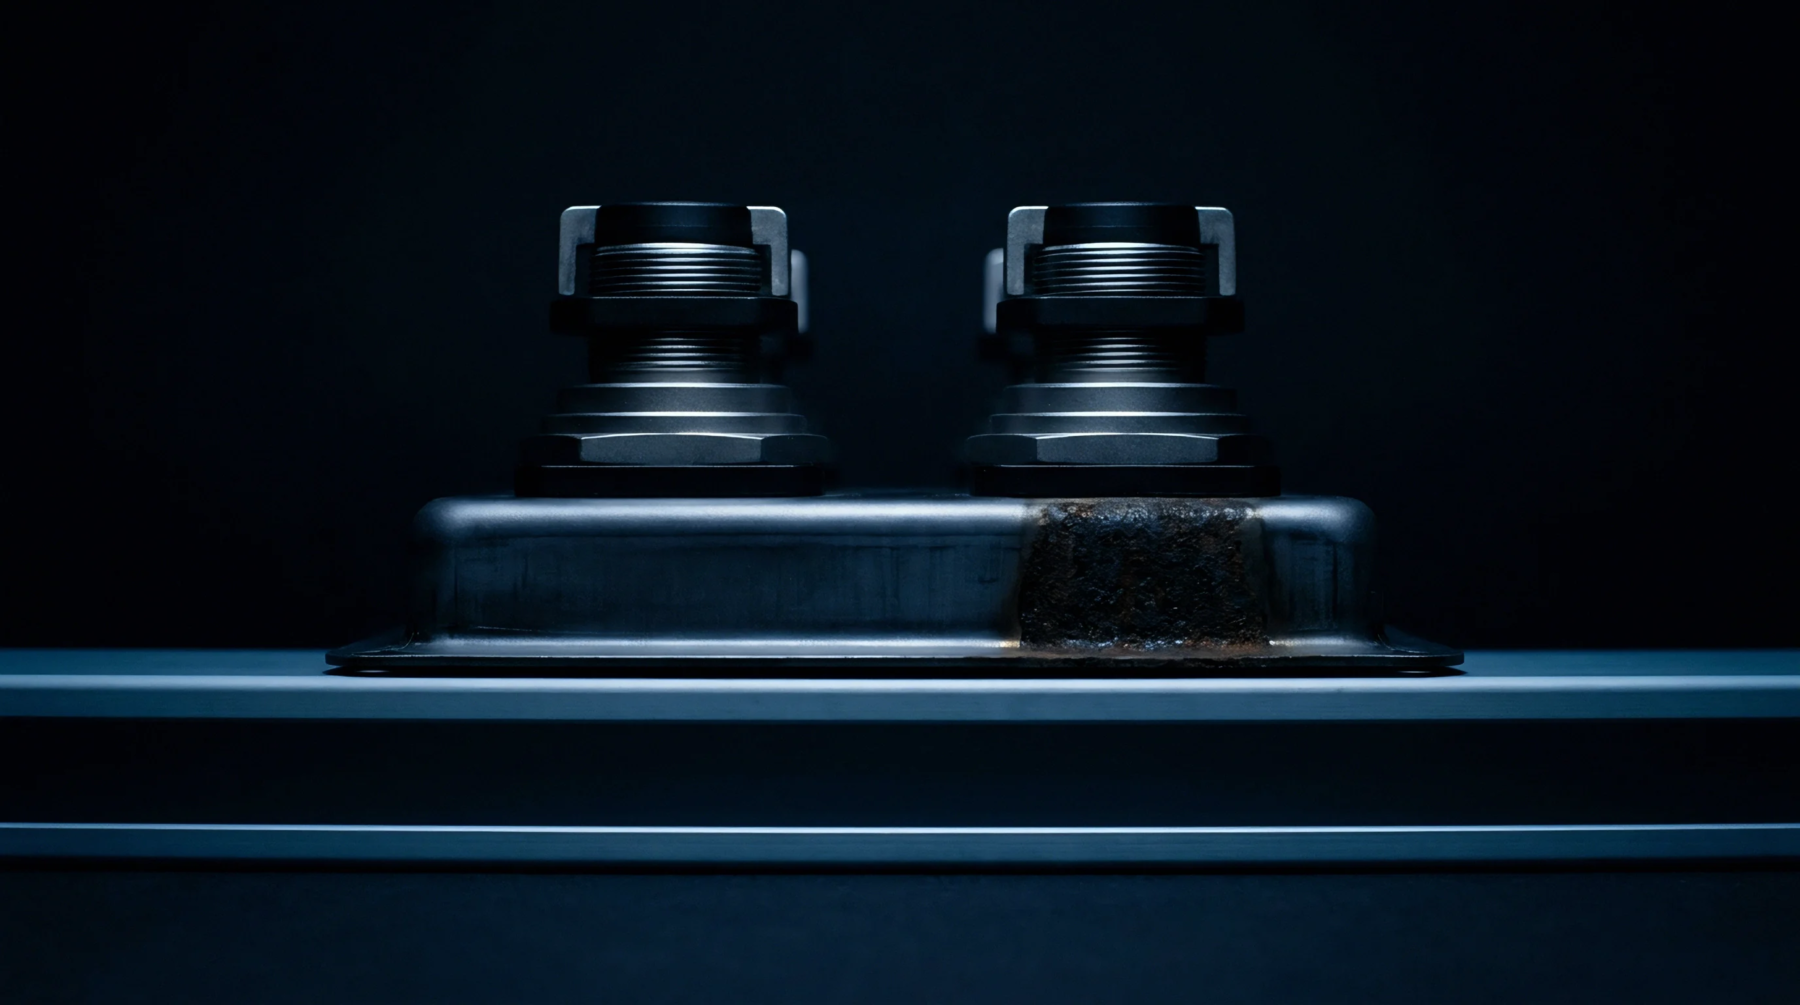
Non-Destructive Testing
Meaning ~ Inspection techniques that evaluate the internal structure of manufactured materials without causing damage represent a formal verification category.
Systematic engineering verification of welded assemblies to confirm compliance with design drawings, welding procedure specifications and contractual quality standards. Rigorous weld inspection encompasses pre-weld fit-up validation, in-process parameter monitoring, post-weld dimensional verification and non-destructive examination for surface and internal discontinuities. The practice governs the structural integrity of fabricated joints in pressure vessels, structural steel, marine hulls and cross-country pipelines.
Its scope terminates at the completed joint and its immediate heat-affected zone, providing no evaluation of parent material properties outside the thermally altered boundary or structural stresses induced by broader civil installations.
Quality control of welded joints begins well before the arc is struck on the production floor. Pre-weld inspection tasks focus on joint geometry, bevel angles, root gap dimensions, surface cleanliness and verification of welder qualification records. During welding, inspectors monitor interpass temperatures, preheat maintenance, heat input calculations and shielding gas flow rates against the qualified welding procedure specification.
In-process surveillance prevents root pass cracking, excessive penetration and metallurgical embrittlement before subsequent passes bury foundational flaws. Neglecting operational surveillance forces expensive gouging and post-weld remediation that could have been avoided through continuous procedural enforcement.
Post-welding evaluation evaluates completed joints against rigid visual, surface and volumetric acceptance criteria. Visual examination screens for surface porosity, undercut, incomplete joint penetration, excessive reinforcement and weld spatter. Non-destructive methods, including magnetic particle, dye penetrant, ultrasonic and radiographic testing, interrogate the weld volume and heat-affected zone for subsurface cracks, slag inclusions and lack of fusion.
Acceptance standards such as AWS D1.1, ASME Section IX or ISO 5817 establish exact numerical allowances for discontinuity size, clustering and location. Joints failing to meet designated quality tiers receive formal non-conformance reports, freezing production until engineering cut-out or repair procedures are authorized.
Execution of welding quality controls dictates factory throughput, payment releases and liability allocations between engineering contractors and fabricators. Failed weld inspection protocols generate severe financial penalties, including rework labor charges, scrapped subassemblies, missed site delivery milestones and liquidated damages. Inspection hold points documented in the inspection and test plan require formal sign-off by buyer representatives before assemblies advance to post-weld heat treatment or painting.
If latent weld defects bypass shop inspections and fail during hydrostatic field testing, the fabricator faces catastrophic remediation costs and warranty liabilities. Comprehensive, auditable weld logs and examination certificates serve as the manufacturer primary legal defense against downstream structural failure claims.
Meaning ~ Inspection techniques that evaluate the internal structure of manufactured materials without causing damage represent a formal verification category.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.