Major Defect
Meaning ~ A quality control category for product deviations that impair functionality or reduce commercial value without introducing safety or regulatory risks.


Bench
A major defect is a manufacturing flaw that degrades a product’s usability or commercial value without creating safety risks or regulatory breaches.
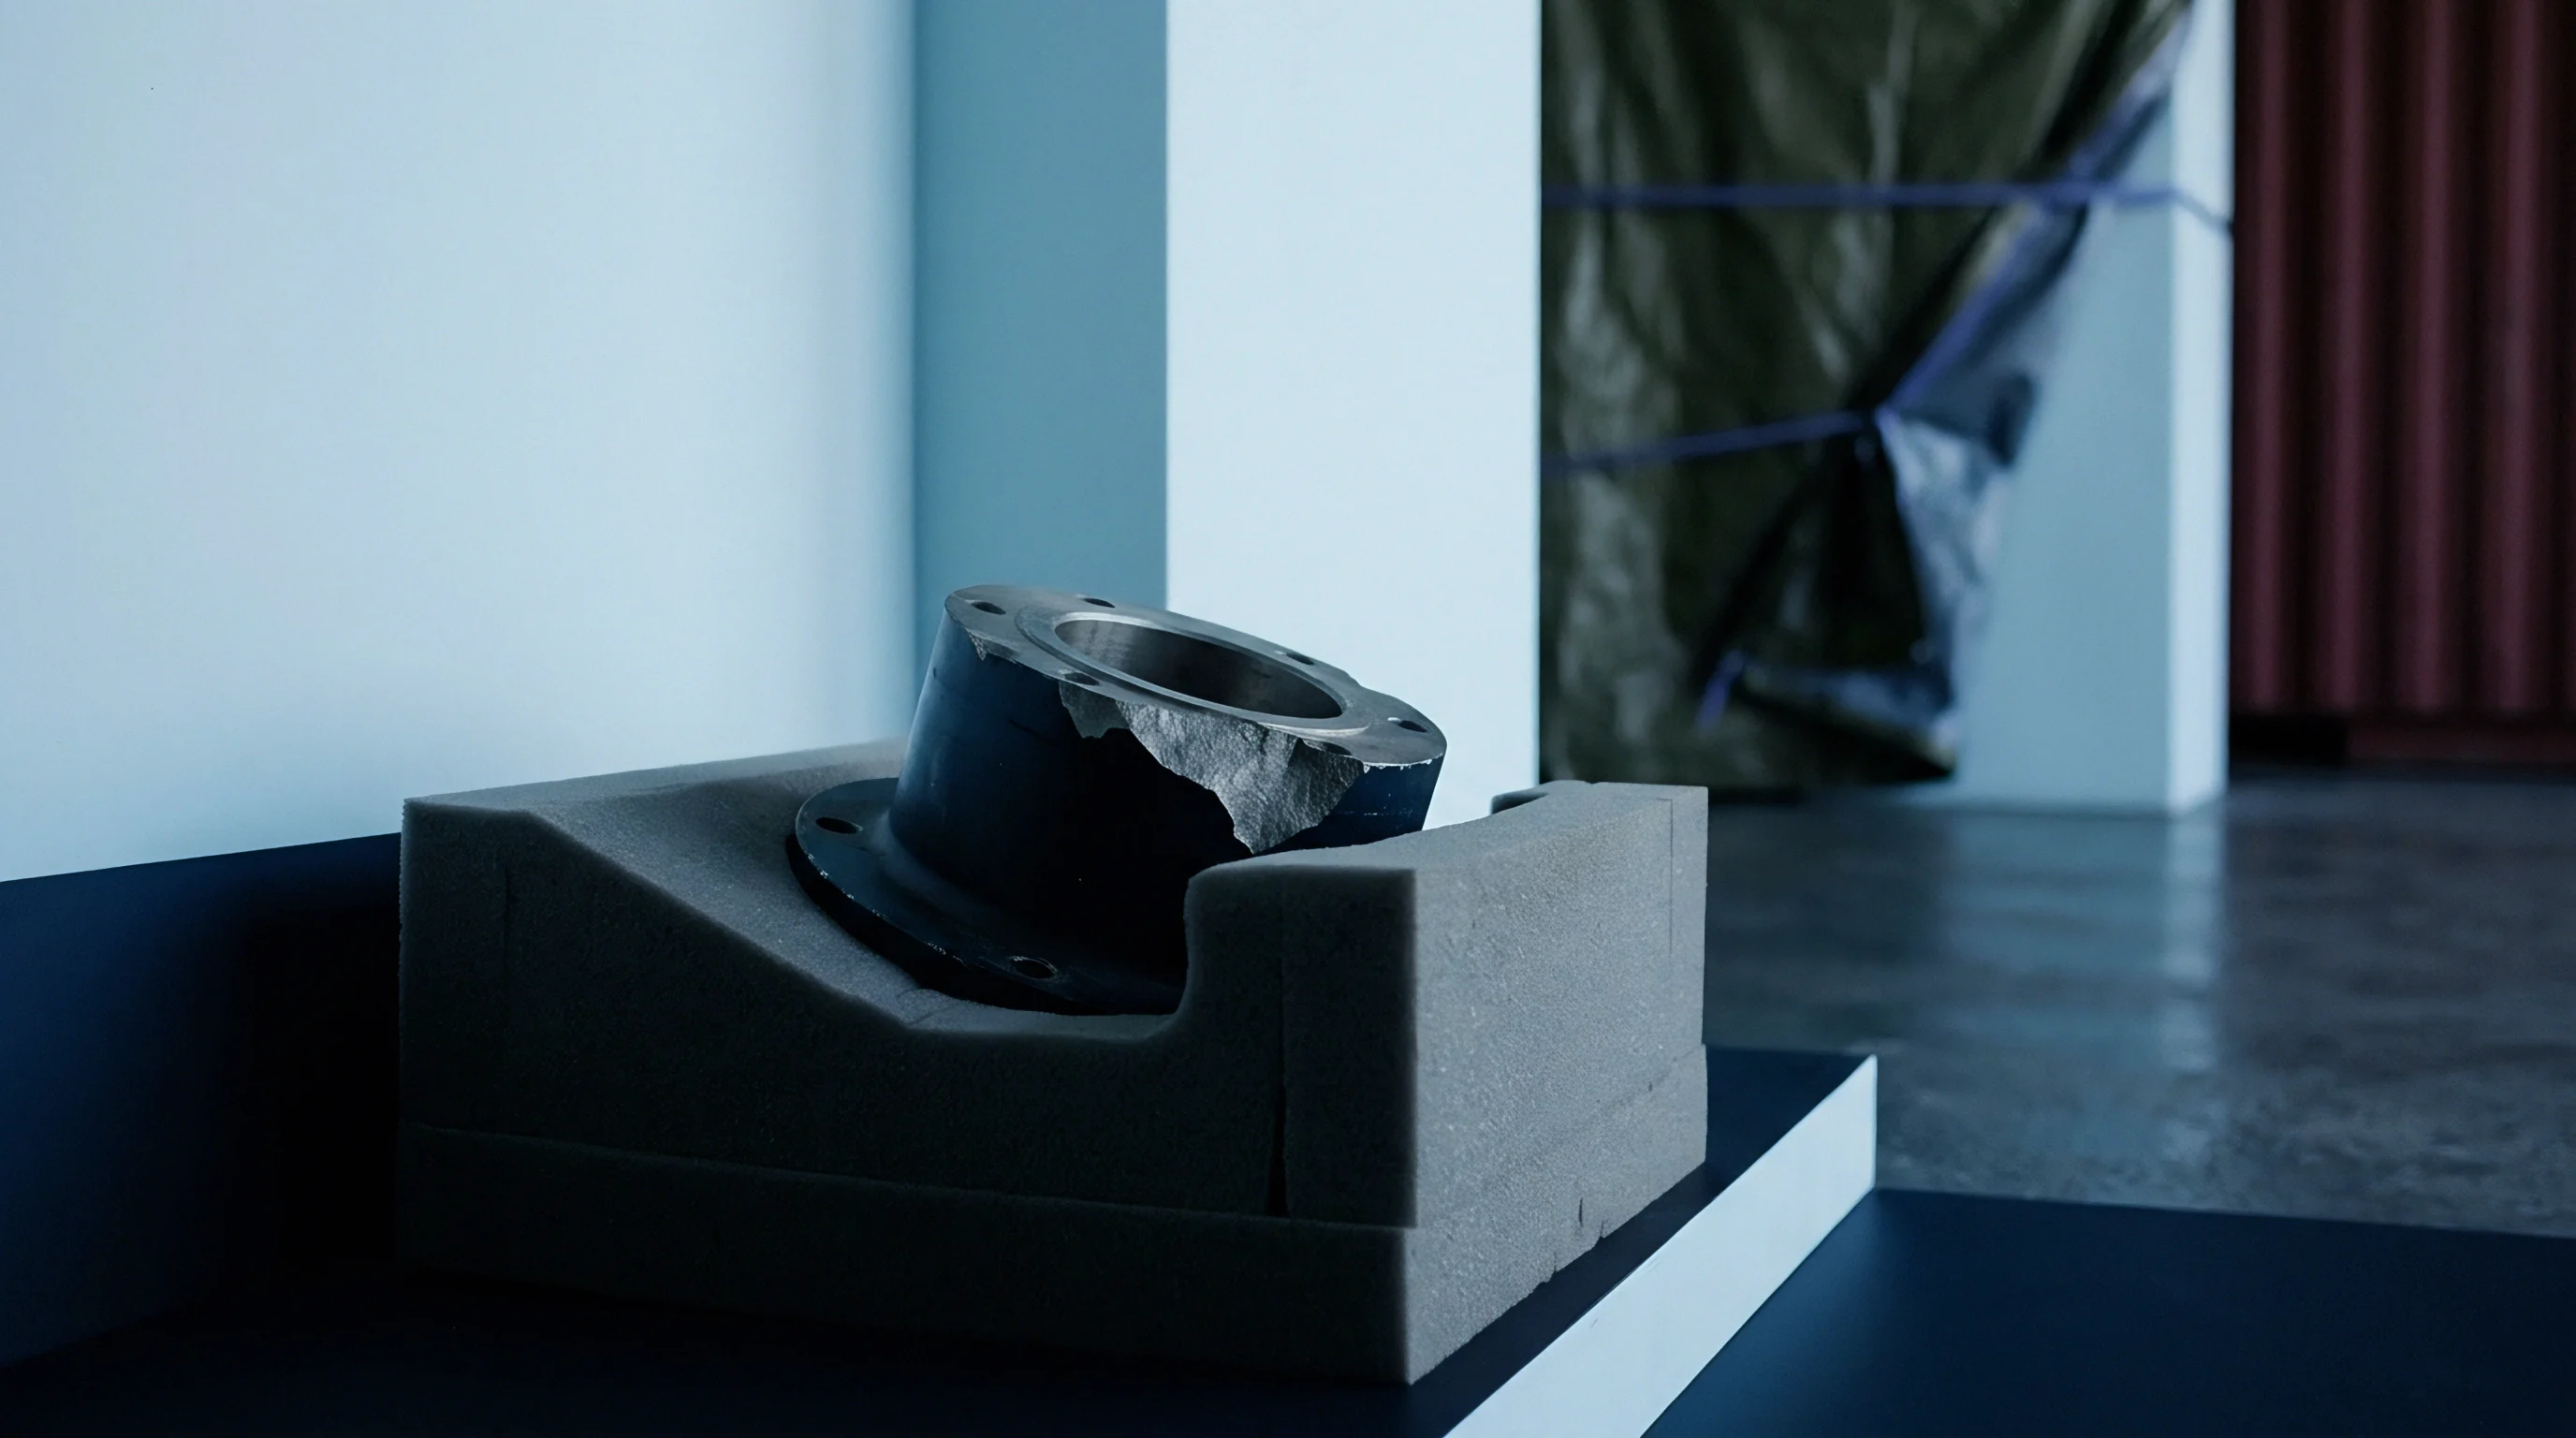
Twelve cracked plastic housings sit on the gray ESD mat, each with a hairline fissure spreading from its brass threaded insert. When the torque driver applied the nominal three Newton-meters of assembly force during product verification, the polycarbonate housing walls fractured immediately. While a cracked casing won’t shock a user or start a fire, it keeps the internal circuit board from mounting securely.
In factory sorting, functional failures like this carry a higher severity rating than cosmetic scratches, though they stay distinct from hazardous defects like an exposed high-voltage wire. That distinction decides whether a batch gets sorted or scrapped outright. The test fixture uses a manual clamp to hold the workpiece beneath a calibrated sensor while the technician logs the deflection angle prior to failure.
If the material fractures under forty percent of its engineered limit, the defect is classified here.
Inspectors on final checks watch for flaws that stop assembly or trigger failures in the field. The line between a cosmetic blemish and a major defect comes down to function: a deep scuff on a housing still holds internal parts together, just as a faded logo button still closes a circuit. Those are cosmetic.
But a button sticking inside its bezel or a casing that lets moisture in directly impairs operation. On the bench, inspectors trace every flaw to its practical impact. Mechanical checks cycle samples through fifty strokes along their working path; if a hinge loses friction or a slider jumps its rail, the inspector logs it.
Those records form the basis for accepting or rejecting the shipment.
Functional Disruption on the Line
Assembly lines operate on tight cycle times, so any part that slows down production gets flagged. A slight variation in screw thread pitch during manual insertion might cost a worker two seconds, but a stripped thread that won’t tighten brings the station to a stop ~ a bottleneck that quickly ripples back across the entire shift. Inspection teams separate these functional blockers from minor workmanship marks.
Physical evidence on the bench consists of finished units failing the functional criteria defined in the quality accord. Tools like feeler gauges, force meters, and digital calipers measure these variances. If an enclosure doesn’t close because of a dimensional error, the inspector logs the gap; anything wider than the specified threshold of one-tenth of a millimeter lets dust in and violates the product’s environmental rating.
Visual checks in standardized light booths pick up defects in molded plastic. A minor color shift turns into a major nonconformity when molding leaves voids or sink marks in structural ribs designed to take mechanical loads. If a sink depth exceeds thirty percent of the wall thickness, the part tends to flex under standard assembly pressure.
Physical torsion testing exposes these weak points by applying torque along the casing’s long axis with a pneumatic arm. If the plastic cracks, the full lot of molded parts goes straight into quarantine.
Classification Boundaries
Setting thresholds for acceptability requires agreement between the sourcing team and the factory. Sourcing frameworks group defects into three tiers to focus inspection effort. Critical defects center on safety and regulatory compliance; a single sharp metal edge or trace of toxic residue grounds the entire shipment.
Minor defects cover cosmetic flaws like faint transit scuffs that won’t hinder retail sales. Major defects sit in the middle: the product is safe to handle, but fails to function as intended. Loose mechanical linkages, incorrect assembly, missing hardware, or dimensional errors that block installation all fall here.
Clear boundaries keep quality managers from wasting time over minor scuffs while ensuring broken units don’t ship.
Physical reference samples help inspectors separate cosmetic blemishes from functional failures. Signed by both engineering and factory management, these limit samples illustrate the worst acceptable finish. If a unit’s surface scratch is deeper than the sample, it gets upgraded from minor to major because the gouge risks compromising the protective coating.
Inspectors use these physical benchmarks on the floor to settle visual disputes against a shared, objective standard.
An experienced inspector looks for where a surface flaw starts to interfere with physical alignment, as that is the exact point where a minor deviation becomes a functional failure.

Sampling
Evaluating a production lot relies on probability models that project total batch quality from a representative subset.
Statistical acceptance plans under ISO 2859-1 define how inspectors select samples and calculate acceptance thresholds. The standard maps lot sizes to specific sample size code letters. Sourcing teams typically default to General Inspection Level II for consumer goods to balance inspection costs against statistical reliability.
For an incoming shipment of five thousand steel hinges, General Level II assigns code letter L, which requires a sample size of two hundred units. These parts are pulled at random across the entire lot to reflect variations in molding runs and cooling cycles throughout the shift.
Inspectors evaluate the sample by comparing the number of defects found against accept and reject limits in the ISO tables. For major defects, the industry default is an Acceptable Quality Limit of 2.5 percent. For code letter L with two hundred units, the table sets an acceptance number of ten and a rejection number of eleven.
Ten or fewer defective units means the lot passes; eleven means it fails. Establishing these hard numbers up front prevents disputes between buyer and supplier.
An on-site inspection fails when more than ten major defects are identified in a random sample of two hundred units drawn from a lot of five thousand pieces.
Random selection follows a set sequence so that every carton has an equal probability of inspection. Checkers use skip-lot intervals or random number lists to pull boxes from pallets. In a fifty-carton shipment, for instance, an inspector might pull four units from each box to build the sample.
Broad sampling stops suppliers from hiding suspect goods in the back of a stack. Factories frequently run into trouble transitioning from pilot runs to mass production, where tool wear and mold temperature swings generate localized pockets of bad parts. Sampling across the full shipment flags those localized clusters before bad inventory gets accepted.
Statistical Framework for Sample Extraction
A sampling plan’s operating characteristic curve shows the probability of accepting a lot across different defect rates. With a sample of two hundred units and an acceptance threshold of ten, the plan almost certainly accepts lots with actual defect rates under one percent. But if the real defect rate hits five percent, acceptance odds plunge below five percent.
That steep curve protects buyers from accepting substandard shipments, while reminding suppliers that sending high-defect batches risks rejection, pressing them to run internal audits before third-party checkers arrive.
When a factory’s quality drops across consecutive shipments, inspections shift from normal to tightened severity. If two out of five consecutive lots fail for major defects, the quality manager enforces tightened inspection: the sample stays at two hundred units, but the acceptance threshold drops from ten to eight. These switching rules maintain pressure on the manufacturer, rewarding consistent quality with lighter sampling while penalizing poor performance with stricter standards.
Acceptance and Rejection Calculation Criteria
Lot compliance rests on a single attribute sampling plan where parts pass or fail with no partial credit. A slightly rough edge on a steel hinge counts as minor, but a bent hinge pin that prevents movement is a functional failure. Inspectors log each defect digitally, attaching photographs alongside caliper readings.
The final count of functional failures dictates lot acceptance, and contracts stipulate that the inspector’s tallies are binding to prevent suppliers from manipulating the sample.
| Lot Quantity Range | General Level I Code | General Level II Code | General Level III Code |
|---|---|---|---|
| 151 to 280 | E | G | H |
| 281 to 500 | F | H | J |
| 501 to 1,200 | G | J | K |
| 1,201 to 3,200 | H | K | L |
| 3,201 to 10,000 | J | L | M |
Master tables in ISO 2859-1 supply the mathematical basis for these plans, eliminating the need to build custom statistical models for every purchase order. Most consumer goods importers accept a standard 2.5 percent threshold for major defects. Higher-precision sectors, such as medical devices, drop that limit to 1.0 percent or lower ~ demanding larger samples and permitting fewer flaws to balance inspection expense against failure risk.
- Major Defect conditions include open solder joints that interrupt current across a PCB.
- Major Defect designations apply to dimensional deviations that fall outside specified assembly tolerances.
- Major Defect anomalies include severe surface oxidation that stops protective coatings from adhering.
- Major Defect criteria include split or frayed insulation exposing conductors where no shock hazard exists.
Faced with a high defect count, factory managers often argue that warehouse humidity spiked that morning, swelling the plastic casings right before the inspector put a gauge to them.

Tolerance
Engineering drawings define allowable variations for every mechanical and dimensional feature of a component.
If tolerances are too loose, individual parts can meet their print specifications yet fail to fit during final assembly ~ a problem known as tolerance stack-up. Sourcing engineers review drawings early to flag dimensions critical to fit and function. For instance, the clearance between a metal bracket and its housing might need to stay under half a millimeter to prevent rattling.
If a worn stamping die increases bracket thickness by two-tenths of a millimeter, the tight fit forces workers to press parts together manually. Tracking these dimensional shifts over a run helps quality teams catch tool wear before it leads to assembly line failures.
Tool wear and mold erosion drive most dimensional drift during manufacturing. As a stamping die hits thousands of sheet metal blanks, its edges round off, throwing larger burrs on part boundaries. Burrs over seventy-five microns high keep brackets from seating correctly in assembly fixtures, skewing alignment.
Inspectors rejected a batch of fifteen thousand anodized aluminum brackets after catching three thread failures during manual checks. An inspector using a calibrated go-no-go gauge found the internal thread pitch had drifted past drawing limits, preventing assembly bolts from turning cleanly.
Engineering Tolerances and Part Alignment
Precision alignment relies on managing stacked tolerances across dissimilar materials. Injection-molded plastic shrinks much more than stamped metal, calling for carefully controlled cooling cycles. When a factory speeds up presses to meet output quotas, parts get ejected early and warp.
Warping shifts mounting boss centerlines so metal brackets no longer align with molded brass inserts. Sourcing contracts often require molded components to sit at room temperature for twenty-four hours before dimensional checking, ensuring parts stabilize before being measured against print.
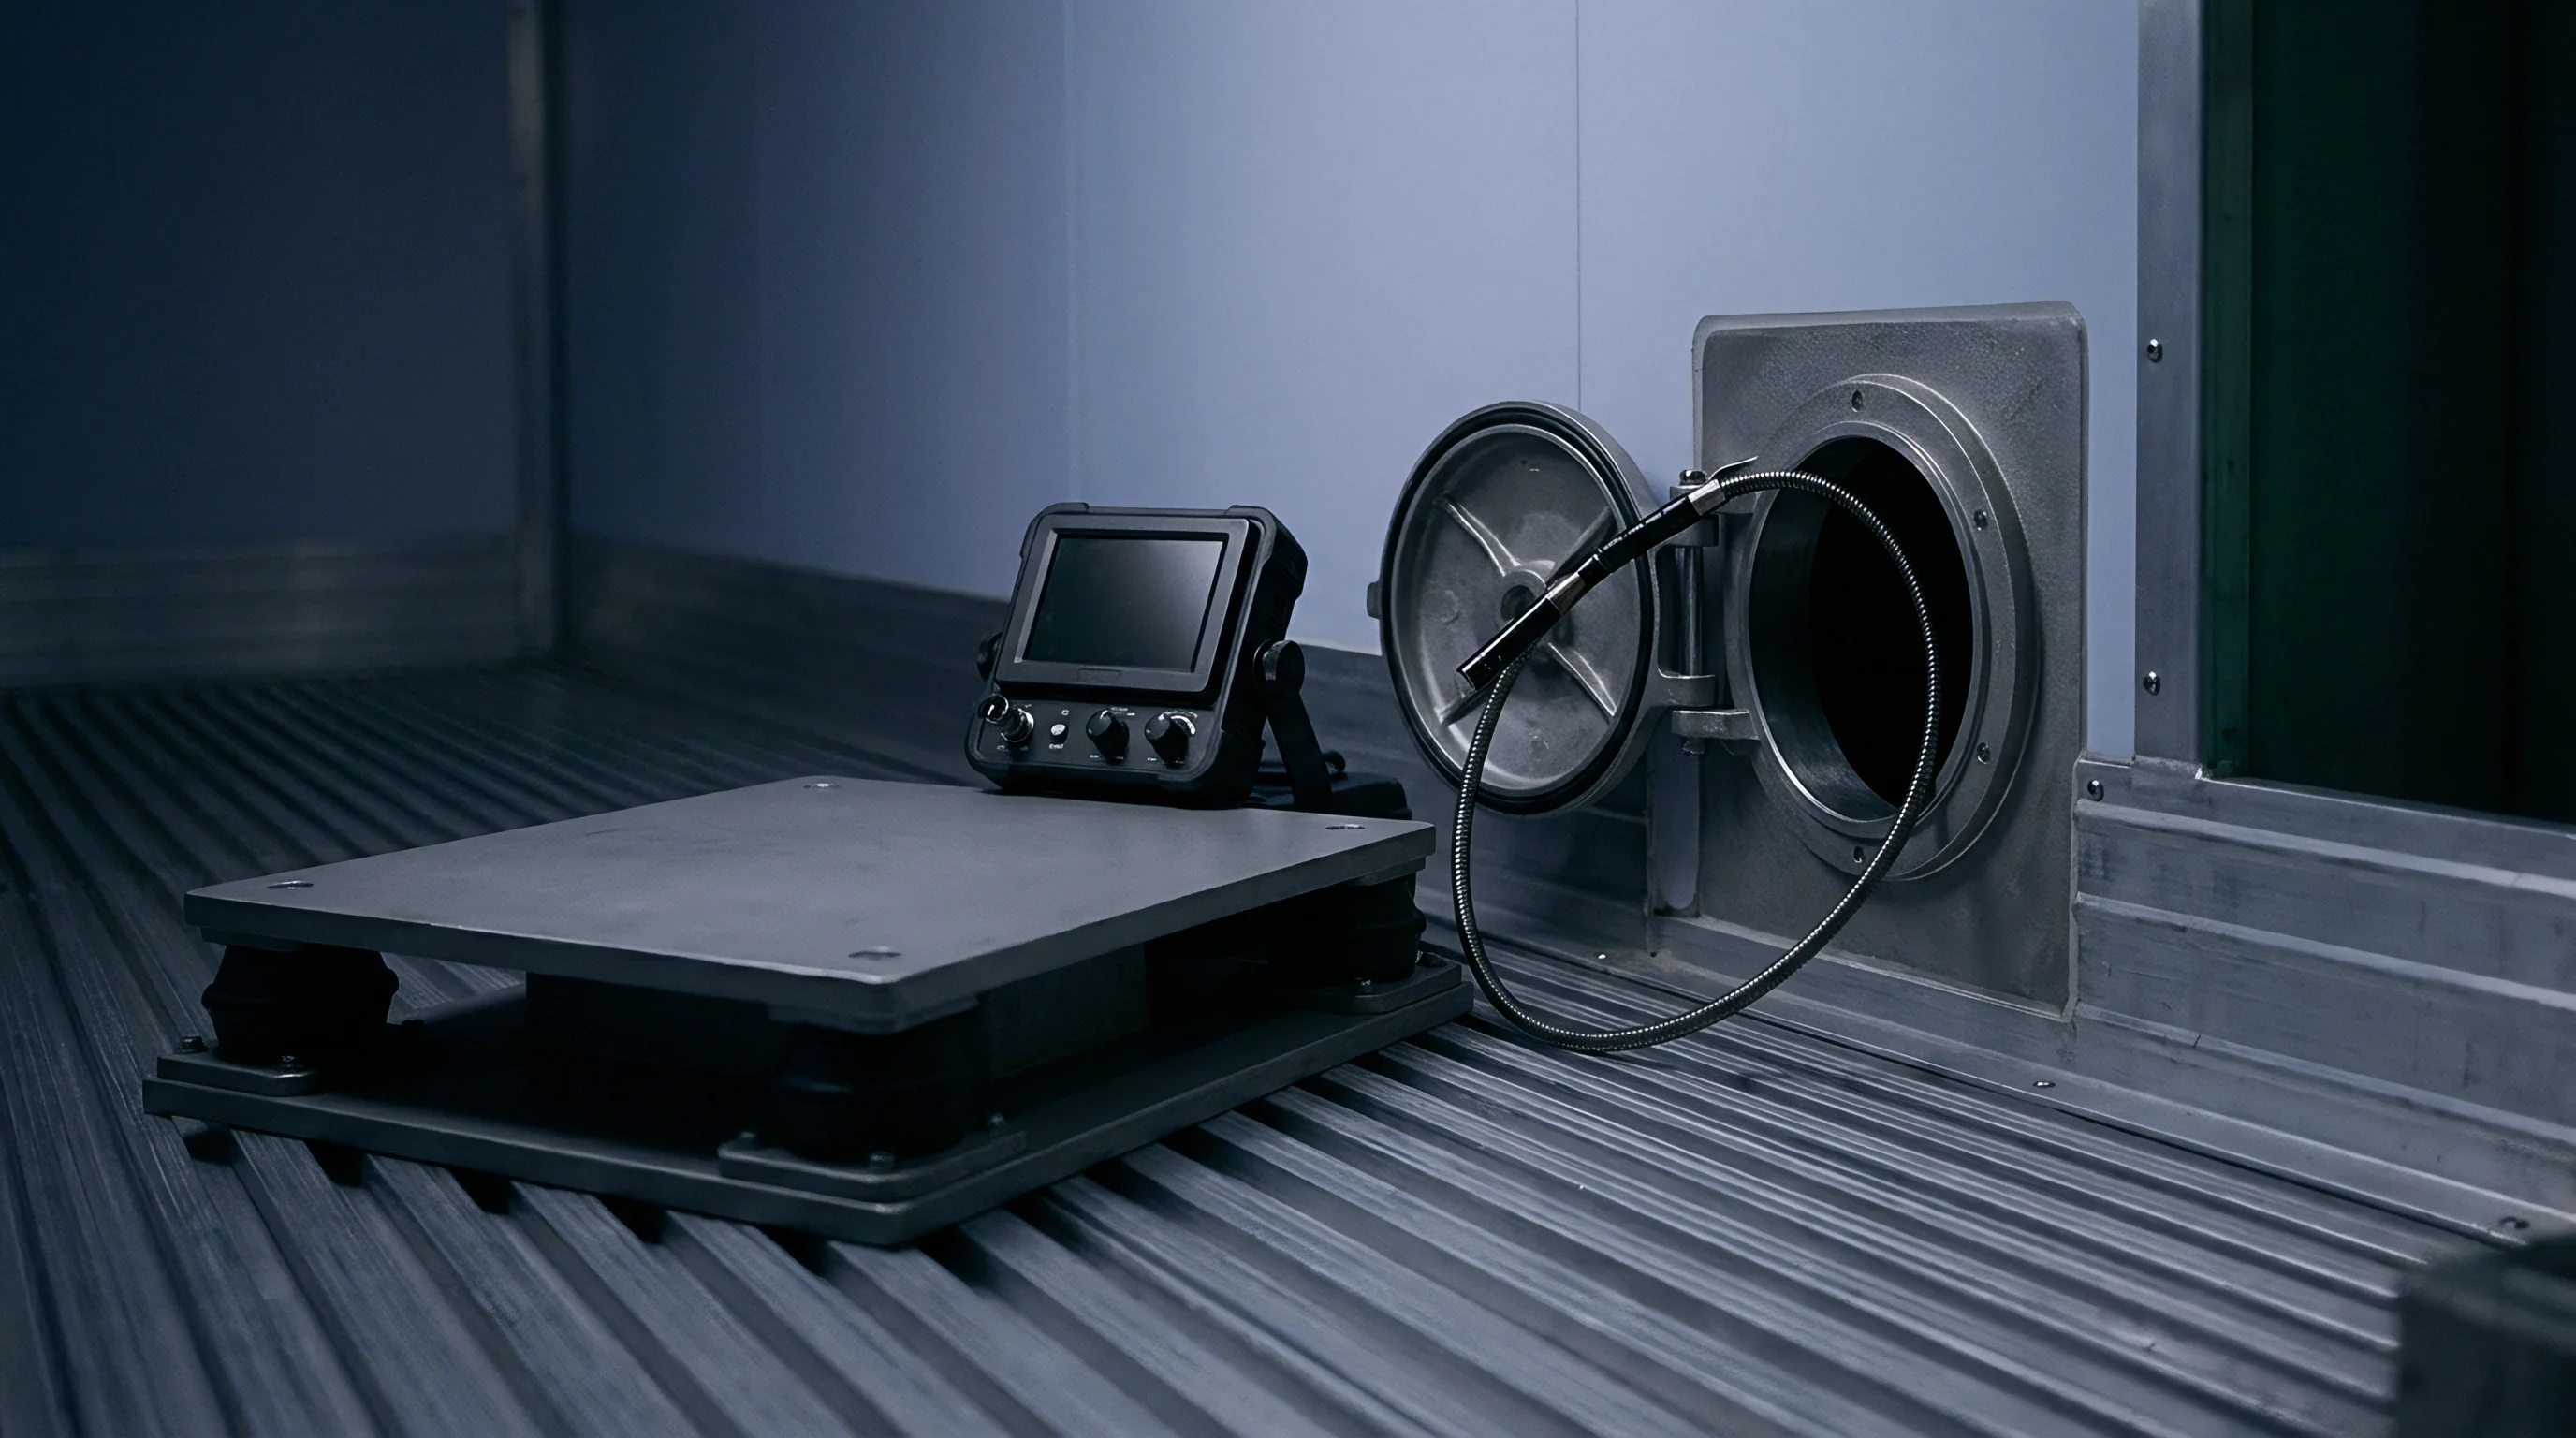
- Mount the calibration fixture to the reference surface.
- Align the force-transducer probe with the load cylinder’s central axis.
- Apply a primary tare force of exactly ten Newtons.
- Record transducer readings across progressive torque steps.
- Check output curve linearity against the factory trace sheet.
Weekly force gauge calibrations keep torque measurements accurate. If a gauge drifts, a tester might log a pass while the assembly is actually being overstressed. Sourcing teams audit these calibration logs quarterly against physical reference weights, ensuring parts aren’t damaged by over-tightening during assembly.
Material Deviation and Tooling Wear
Raw material variance also alters part dimensions during production. Ultrasonic horns press brass inserts into polycarbonate housings; if a brass shipment has higher lead content than specified, the softer metal deforms under insertion force. Contracts specify alloy compositions and require material test reports for every batch sent to the shop.
When test results deviate, the factory must pause the line and adjust horn settings to prevent cracking the housing walls.
Molding tools lose clean edges over long production runs, allowing flash to creep along parting lines. When flash along an edge exceeds three-tenths of a millimeter, it stops the part from sitting flush in assembly jigs. Workers then have to trim flash by hand ~ adding labor cost and risking accidental gouges.
Sourcing auditors flag manual deburring stations because they signal worn tooling that needs re-machining.
On high-precision plastic enclosures, failing to specify draft angle tolerances before tooling cut-off resulted in three thousand dollars in expedited air freight charges.

Contract
Purchase agreements and quality accords convert statistical limits into legally binding terms for both manufacturer and buyer.
Quality accords detail defect categories, sample sizes, and financial remedies for inspection failures. Modern contracts tie final balance release directly to a passed pre-shipment inspection report. If defect counts cross the rejection threshold, final payment is withheld, giving the buyer leverage to insist on full sorting or a complete production rerun.
Cross-border purchase terms standardly use a thirty percent deposit with the seventy percent balance released against a passed inspection certificate and bill of lading. This splits commercial risk between parties. If major defects breach the AQL limit, the supplier cannot claim the balance until the issue is rectified.
Contracts set firm timelines for resolving failures, making the factory responsible for sorting costs and re-inspection fees.
Under Section 8.4 of the typical cross-border supply contract, the emergence of more than ten major defects in a sample of two hundred units forces the supplier to cover the full cost of a secondary inspection.
Buyers should finalize defect classifications before sending the initial deposit. If an accord leaves a defect’s severity ambiguous, factories will lobby for a minor rating to avoid lot rejection. Detailed defect catalogs signed by engineers from both companies and appended to the contract eliminate guesswork for third-party inspection teams.

Contractual Integration of Quality Agreements
Supply contracts set the legal framework for cross-border quality control, naming the inspection site ~ usually the factory floor or a consolidation warehouse ~ before container loading. Buyers pay for initial checks by independent third-party agencies, but if a lot fails for excess defects, re-inspection costs shift to the supplier, creating a clear financial incentive to produce conforming goods.
Contracts should clearly lay out remedies when a shipment fails. Typical clauses require the supplier to sort the lot within a set number of days or, if sorting isn’t feasible, re-run production at their own expense using fresh raw material. Late-delivery penalties associated with rework cushion the buyer against missed retail launch dates.
- Major Defect liabilities shift entirely to the contractor when pre-shipment checks fail.
- Major Defect logs must be filed within forty-eight hours of sampling.
- Major Defect chargeback rates tie directly to bill-of-materials costs.
- Major Defect settlements require the factory to fund sorting or build replacement runs.

Legal Remedies for Repeated Failures
Persistent failure to meet quality standards constitutes a material contract breach, allowing the buyer to terminate the agreement. Contracts outline escalation steps ~ starting with formal corrective action plans and leading to purchase order cancellation and deposit refunds. If a supplier fails to address root causes, tooling recovery clauses let the buyer retrieve molds and fixtures to transfer production to another facility.
Warranty clauses address latent defects discovered after customs clearance and retail distribution. If systemic flaws bypass pre-shipment sampling, contracts require suppliers to cover unit replacement, return freight, and administrative costs. Standard warranty protection runs for twelve months post-delivery.
Under standard indemnity provisions, if the defect count reaches double the allowed threshold, the factory must sort the entire batch within ten calendar days or face a freeze on the balance of their letter of credit.

Friction
Quality disputes on the floor usually break out over borderline units.
When an inspector points out a scratch on a steel bracket, factory managers naturally argue it has zero impact on structural strength. Clear photos of obvious defects rarely draw arguments, but gray-area flaws trigger intense debate. Quality protocols defuse these standoffs with objective tests ~ such as cross-hatch adhesion checks or drop tests ~ that demonstrate whether a blemish compromises part durability.
Inspection conditions themselves can spark arguments. Contracts often mandate checking parts in a standardized D65 light booth to maintain uniform illumination. Dim warehouse lighting hides hairline fractures that later turn into field failures, so inspectors insist on evaluating parts inside the booth rather than on shadowy factory floors.
Factories routinely dispute the classification of surface abrasions, arguing they do not affect functional performance.
Factories pressed for time often try to rush inspections to meet container loading cutoffs. Contracts prevent this by requiring inspection approval prior to booking container space, giving buyers time to review findings. Loading goods before receiving a report breaches the accord, allowing buyers to reject the shipment out of hand and preventing suppliers from using shipping deadlines to force acceptance.
What Happens When a Shipment Fails?
When an inspection fails, suppliers almost always start by challenging the defect tally. Reviewing high-resolution defect photos together usually settles the argument quickly when broken brackets or dead circuits are clearly visible. Once the failure is conceded, the factory must submit a Corrective and Preventive Action (CAPA) report detailing root causes and production fixes for future runs.
If arguments continue, teams pull a secondary, larger sample or send samples to an accredited lab. Escalation is slow and costly, and contracts penalize frivolous disputes by charging all testing and freight fees to the losing party.
Dispute Resolution on the Floor
Floor disputes demand both technical firmness and diplomacy. If a factory manager insists a dimensional offset is acceptable, an inspector demonstrates the issue right on the bench. If mating parts won’t fit without brute force, the offset is demonstrably major ~ overriding whatever internal drawings the factory presents.
Digital tracking logs document every dispute and resolution over time. These records feed supplier scorecards, and factories that repeatedly contest valid rejections risk disqualification from future orders.
It remains to be seen whether arbitration boards will continue relying primarily on physical return rates or accept digital inspection photos as conclusive legal proof of product failure.

Money
The true cost of product failures goes far beyond the replacement value of bad parts.
When a lot fails inspection, expenses quickly rack up: sorting labor, rework, tied-up warehouse capacity, and schedule delays. If defective goods slip through to market, costs multiply through return freight, retail chargebacks, and brand damage. Quality control budgets are calculated to keep inspection overhead comfortably below the projected cost of field failures.
Rework economics depend on where and how repairs happen. Sorting and repairing units at the origin factory carries lower labor rates paid by the supplier. Doing the same work at a destination warehouse under local labor rates can easily exceed the original unit cost.
Contracts allocate these expenses upfront, holding suppliers liable for destination sorting, third-party warehousing, and local labor.
Scrap Rates and Financial Recovery
Scrap rates directly drive unit costs in molding and stamping. Non-reworkable functional defects get scrapped, wasting raw material. Purchase contracts build a standard scrap allowance into unit pricing, requiring suppliers to absorb material costs above that threshold.
Tracking scrap rates highlights plants struggling with process control, where high scrap numbers routinely cause production delays as factories over-run batches to hit order quantities.
| Detected Defect Rate | Lot Status | Rework Hours | Scrap and Tooling Expense | Landed Unit Cost Shift |
|---|---|---|---|---|
| 1.2% | Accepted (Under Threshold) | 14 Hours | 350 USD | +0.05 USD |
| 3.5% | Rejected (Failed Inspection) | 120 Hours | 2,450 USD | +0.38 USD |
| 6.8% | Full Rejection (Total Remake) | 450 Hours | 8,900 USD | +1.45 USD |
| Methodology: Rework calculations assume a base labor rate of 25 USD per hour with a fixed lot size of 5,000 polycarbonate housings. | ||||
Financial recovery mechanisms should be spelled out in the contract to ensure swift resolution. Buyers issue debit notes to deduct inspection fees and sorting costs directly from final balance payments, avoiding lengthy negotiations over cash refunds.

Rework Labor Economics
Deciding whether to rework a failed lot comes down to comparing fixed and variable expenses. Fixed costs cover new assembly jigs or retooling machines; variable costs include labor wages and replacement parts. Sourcing managers weigh these factors when deciding between approving a rework plan or demanding a full re-run ~ which takes longer, but often yields cleaner finished goods.
Contracts specify how reworked lots get evaluated prior to release. Any reprocessed batch must undergo full re-inspection under tightened criteria to confirm the rework didn’t introduce new flaws. The factory pays for re-inspection, reinforcing the incentive to maintain quality on the initial run.
As factories shift from manual inspection to automated machine vision, quality economics move from variable labor hours to fixed investments in hardware and calibration software.